
What was actually run.
PQR
PROCEDURE QUALIFICATION RECORD
The PQR is proof your welding procedure works. It records exactly how the test coupon was welded, and how it held up when we tested it. Your WPS is built on it.
The ingredients. Exactly what went into the test batch, and how it came out.
THE THREE PAPERS
PQR, WPS, WPQ: what's the difference?
They get mixed up all the time. Each one answers a different question.
PQR
The ingredients- Answers
- Does this procedure make a sound weld?
- Records
- The actual values used on one test coupon
- Changes?
- No. It's a record of what happened.
WPS
The recipe- Answers
- How should the shop weld this joint?
- Records
- Allowed ranges, backed by the PQR
- Changes?
- Can be revised, within what the PQR supports.
WPQ
The chef- Answers
- Can this welder follow the WPS?
- Records
- One welder's test and what they're qualified for
- Changes?
- Kept current by the welder's continuity.
WHAT'S ON A PQR
Read a PQR in two minutes
The top half is what was run. The bottom half is how it tested. Here's what each section means.

- WHAT WAS RUN · PAGE 1
- 01
Joint
QW-402The groove shape: bevel angle, root opening, backing or not.
- 02
Base metal
QW-403What the coupon was made of, and how thick.
- 03
Filler metal
QW-404The rod or wire used, by spec and classification.
- 04
Position
QW-405How the coupon was held: flat, vertical, overhead.
- 05
Heat
QW-406 · 407Preheat before welding, and any heat treatment after.
- 06
Gas, electrical, technique
QW-408 · 409 · 410Shielding gas, amps and volts, travel speed, stringer or weave.
- HOW IT TESTED · PAGE 2
- 07
Tensile test
QW-150Strips pulled until they break. Shows the weld is as strong as the metal.
- 08
Guided bend test
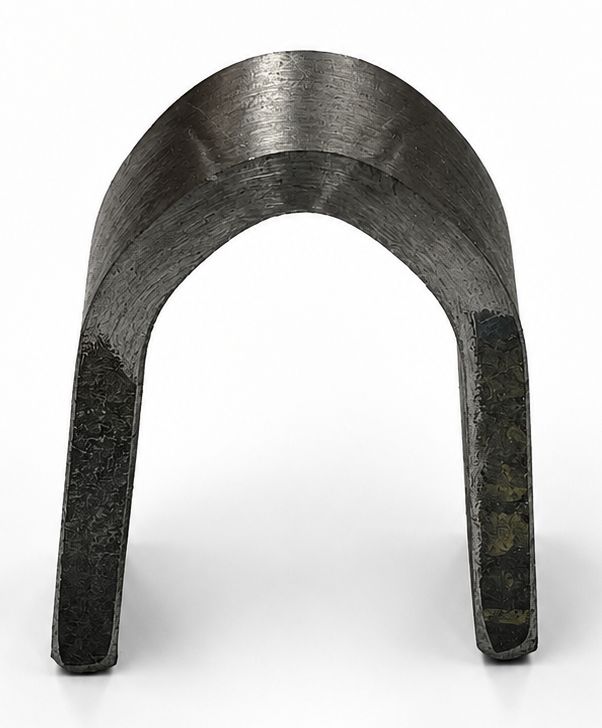
QW-160Strips folded into a U. Shows the weld isn't hiding flaws.
- 09
Certification
Signed off by the company that ran the procedure. That signature makes it official.
HOW A PQR GETS MADE
From coupon to record
TQT writes the record from the coupon.
-
We cut and test
Tensile and bend strips from the coupon.
TQT -
We write the PQR
Settings plus results, on one record.
TQT -
You certify it
Your company signs it. Now it's yours.
You
THE TESTS
How a coupon proves itself
Two tests do most of the work.
Tensile
A strip across the weld is pulled until it breaks. The machine records the force.
PASSMeets the minimum strength of the base metal.
Guided bend
A strip is bent around a die into a U. Any hidden flaw opens up on the outside.
PASSNo open flaw over 1/8" in any direction.
GOOD TO KNOW
What a PQR is not
Not a welder's card
It qualifies the procedure, not the person. Welders qualify with a WPQ.
Not something you edit
It records what happened. Change an essential variable and you need a new PQR.
Not one-per-job
One PQR can support more than one WPS, within its ranges.
Turnaround
How fast you get your PQR
Typical turnaround is 5–7 days. Need it sooner? Add expedite or rush.
Ask for expedite or rush when you book or call.
QUESTIONS
Before you start
Does a PQR expire?
Under ASME Section IX, no. It stays valid as long as the procedure doesn't change beyond what it covers.
Do I need a PQR at all?
Under ASME Section IX, yes. Under AWS D1.1, prequalified procedures can skip it. Not sure which applies to you? Call us.
How long does it take?
Typically 5–7 days. Expedite (3–5 days, +$50) and rush (1–2 days, +$200) are available.
What do I need to record while welding the coupon?
Amps, volts, travel speed, preheat, filler, gas and position. Record them as you weld, then fill out the TQT Welder Qualification Form and send it with the coupon.
Need a procedure qualified?
Tell us the joint and the code. We'll plan the coupon.